
Sulzer products supplier
Sulzer Pump Sales
Sulzer is a globally recognised engineering company with a long history in fluid handling technology. Its involvement in pump manufacturing dates back to the nineteenth century, and it has developed an extensive range of equipment for industries where the movement and management of liquids are essential to everyday operations.
Unlike manufacturers that concentrate primarily on domestic water supply or building services, Sulzer has a strong focus on demanding industrial processes. Its pumping solutions are used in sectors including water and wastewater treatment, chemical processing, oil and gas, power generation, manufacturing and pulp and paper production.
The Sulzer portfolio includes centrifugal process pumps, submersible wastewater pumps, progressing cavity pumps, sludge transfer equipment and specialist high-capacity pumping systems. Beyond pumps, the company also manufactures industrial mixers, agitators, compressors and aeration equipment.
Whats for sale?
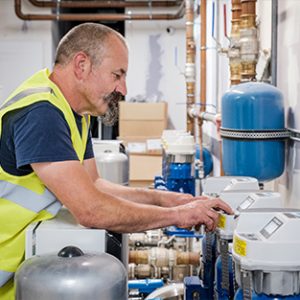
Sulzer Booster Pumps
Sulzer manufactures a range of booster pumps designed to increase pressure and maintain the movement of liquids across demanding industrial and infrastructure applications. Its portfolio includes high-pressure process boosters, multistage pumps and large-capacity pumping solutions for applications such as water transportation, desalination, boiler feed systems and industrial processing. Sulzer also supplies specialist booster pumping equipment for large-scale water systems.
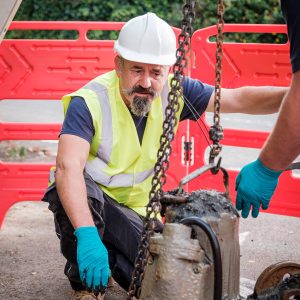
Sulzer Submersible Wastewater Pumps
Sulzer's submersible wastewater portfolio includes pumps designed to operate in demanding sewage and effluent applications. The range incorporates different hydraulic designs to handle liquids containing solids, fibrous materials and other contaminants. Its XFP range includes submersible wastewater pumps for municipal and industrial applications. Depending on the model and configuration, these pumps can be used in sewage pumping stations and wastewater treatment.
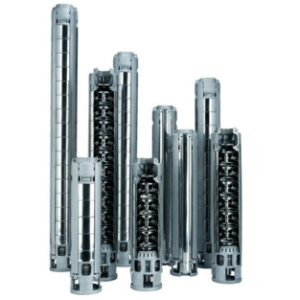
Sulzer Borehole Pumps
Sulzer manufactures specialist borehole and deep-well pumping solutions designed to extract water from significant depths and support demanding water supply applications. Its SJT vertical pump range is engineered to lift water from underground sources, including deep wells and groundwater reserves, offering an efficient and dependable solution for large-scale water abstraction. These pumps are suited to applications where reliable water extraction is essential, including municipal water supplies, industrial facilities and infrastructure projects. With a focus on hydraulic performance, operational efficiency and long-term reliability, Sulzer's deep-well pumping technology provides solutions for challenging water intake requirements.

Sulzer Dewatering Pumps
Sulzer also manufactures submersible dewatering pumps for removing unwanted water from industrial and construction environments. These pumps are designed for applications such as excavation drainage, groundwater removal, industrial site drainage and other situations where water needs to be extracted from below ground level or confined areas.
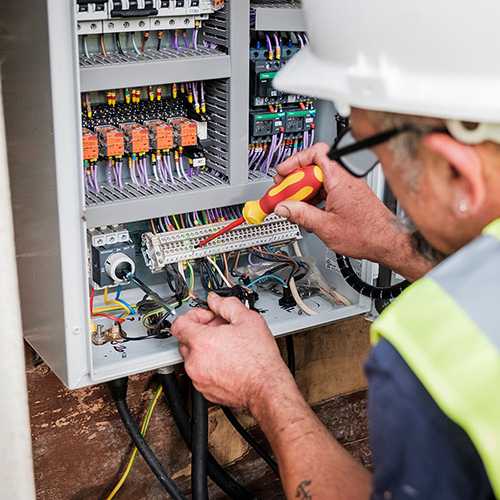
Sulzer Control Panels
Sulzer offers a comprehensive range of pump control panels designed to manage, protect and optimise pumping equipment across a variety of applications. Its ABS control panel range includes compact solutions for single- and twin-pump installations, alongside more advanced systems for larger pumping stations. Models such as the CP 114, CP 112 and CP 212 provide pump operation management and protective functions, including overload, overheating and dry-running protection.
Why buy from us?
Peace of Mind
When you purchase a Sulzer pump through Mawdsleys Pump Services, you can benefit from the applicable manufacturer's warranty, subject to the relevant terms and conditions.
If an issue arises with your equipment, our team can help explain the next steps and provide guidance on the warranty process where appropriate. We aim to make sure customers have access to knowledgeable assistance after their purchase, as well as when choosing their equipment.
24/7 Emergency Pump Breakdown Support
In industrial environments, a pump failure can affect much more than the pumping system itself. It can interrupt production, disrupt essential processes and create problems for the wider facility.
Mawdsleys Pump Services provides emergency pump breakdown support 24 hours a day, 7 days a week, 365 days a year. If your Sulzer pumping equipment develops a fault, our team can assist with the next steps and prioritise emergency breakdown requirements.
We understand that operational downtime can be costly, which is why having access to responsive engineering support is an important part of managing critical pumping equipment.
Experienced Engineers
Industrial pumping applications often require careful consideration of fluid characteristics, system pressures, flow requirements and operating conditions. A pump that is suitable for one process may be entirely inappropriate for another.
The experienced engineers at Mawdsleys Pump Services can help customers assess their requirements and identify suitable pumping equipment. Whether you are replacing an existing Sulzer pump, reviewing an industrial installation or sourcing equipment for a new project, we can provide practical advice.
Our engineering capabilities also extend beyond equipment supply, with installation, servicing, maintenance and fault diagnosis available to help support the ongoing operation of your pumping systems.


Sulzer Pumps Sales FAQs
Sulzer manufactures pumping equipment for a wide range of industrial sectors, including water and wastewater treatment, oil and gas, chemical processing, power generation, pulp and paper, and general manufacturing. Its portfolio includes specialist equipment for processes involving clean water, wastewater, sludge, chemicals and other industrial liquids.
A centrifugal pump uses an impeller to transfer energy to the liquid, making it suitable for many water and general fluid-transfer applications. A progressing cavity pump uses a rotating rotor within an elastomeric stator to move liquid through a series of cavities. This positive displacement design is particularly useful for viscous liquids, sludge and certain types of slurry. The right technology depends on the fluid and the demands of the application.
Sulzer offers specialist industrial pumping solutions for applications involving challenging liquids. Different pump designs, materials and sealing arrangements are available depending on the fluid characteristics. However, not every pump is suitable for abrasive or corrosive duties. The liquid’s chemical composition, temperature, solids content and operating conditions should all be considered before selecting equipment.
Sulzer AHLSTAR pumps are centrifugal process pumps designed for industrial applications. They are used for transferring process liquids and water in sectors such as manufacturing, chemical processing and water treatment. The appropriate model depends on the required hydraulic performance and the characteristics of the liquid being pumped.
The most suitable pump depends on the sludge’s viscosity, solids concentration, abrasiveness and required transfer rate. Sulzer offers several technologies for sludge applications, including progressing cavity pumps and specialist submersible sludge pumps. A proper assessment of the material and installation is important before selecting a model.
Sulzer manufactures equipment for many industrial processes where pumps are expected to operate for extended periods. However, suitability for continuous operation depends on the specific model, duty point, liquid being pumped and installation conditions. Correct specification and appropriate maintenance are important for achieving reliable performance.
The original model reference and pump rating plate are useful starting points. Additional information may include the required flow rate, delivery head, motor power, speed, liquid characteristics, connection sizes and installation arrangement. For process applications, details about the liquid’s temperature, viscosity and solids content can also be important.