
Mono products supplier
Mono Pump Sales
Mono is a recognised manufacturer of progressing cavity pumps and specialist fluid-handling equipment, with a history dating back to 1935. Now part of NOV, the brand has built its reputation around pumping technology designed to handle challenging liquids and demanding industrial processes.
Unlike manufacturers whose ranges focus primarily on conventional centrifugal pumps, Mono specialises in positive displacement technology. Its progressing cavity pumps are particularly suited to applications involving viscous liquids, slurries, sludge and products containing solids, where maintaining a consistent flow is important.
The Mono portfolio also includes macerators, grinders, screening equipment and packaged pumping systems. These products are used across industries including water and wastewater treatment, food and beverage production, chemical processing, mining, agriculture and oil and gas.
Whats for sale?
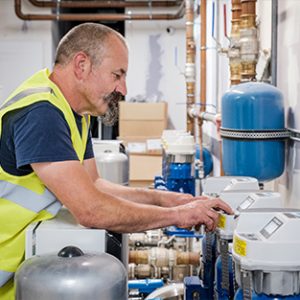
Mono Booster Pumps
Mono provides pumping solutions for water supply and treatment systems where increasing pressure or transferring water to a higher point is required. Its wider portfolio includes packaged water-treatment and pumping systems incorporating booster pumps, pipework and electrical control equipment. These arrangements can be used in applications such as treated-water distribution, irrigation and industrial processes.
Mono Sewage Pumps
Mono has extensive experience in wastewater handling, providing pumping and solids-management equipment for sewage treatment and wastewater processing applications. Its progressing cavity pumps are particularly useful for transferring sludge and other challenging materials, while its Muncher macerators reduce larger solids and fibrous matter to help protect downstream equipment.
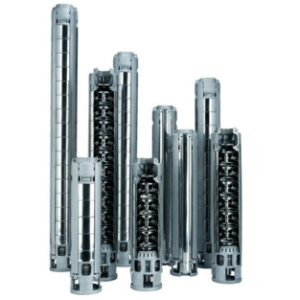
Mono Booster Pumps
Mono provides pumping solutions for water supply and treatment systems where increasing pressure or transferring water to a higher point is required. Its wider portfolio includes packaged water-treatment and pumping systems incorporating booster pumps, pipework and electrical control equipment. These arrangements can be used in applications such as treated-water distribution, irrigation and industrial processes.

Mono Dewatering Pumps
Mono's Subrotor range includes submersible borehole pumping technology designed to extract potable water from underground sources. The pump and electric submersible motor are installed below the water level, allowing water to be delivered from the borehole to the surface. These systems are available in different configurations to suit borehole dimensions and electrical requirements. For installations involving significant sand or abrasive content, Mono also offers alternative borehole pump arrangements designed for these conditions.
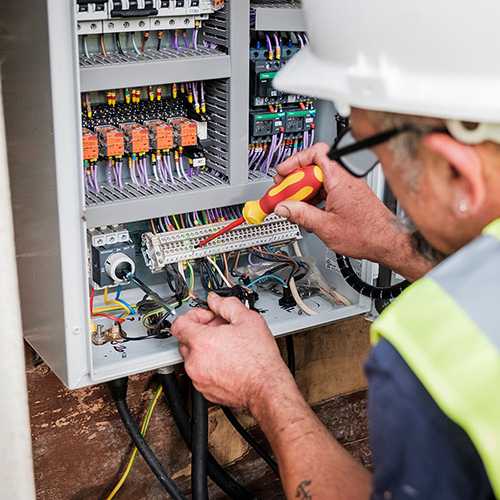
Mono Control Panels and Pump Controllers
Mono offers electrical control equipment and accessories to support the operation of its pumping systems. For its Subrotor borehole pumps, available accessories include single-phase control boxes, three-phase direct-on-line starters and level controllers. These components help manage pump operation and provide the necessary electrical protection for the motor. Control requirements vary according to the pump size, power supply and installation, so the correct equipment should be selected to match the individual system.
Why buy from us?
Manufacturer's Warranty and Peace of Mind
When you purchase a Mono pump through Mawdsleys Pump Services, your equipment benefits from the applicable manufacturer's warranty, subject to the relevant terms and conditions. Should you have a warranty query, our team can help explain the next steps and provide guidance where required.
Priority Pump Breakdown Support
Unexpected pump failure can have a serious impact on production, wastewater operations and essential site processes. Mawdsleys Pump Services provides a 24/7 emergency pump breakdown service, 365 days a year, giving customers access to support when an urgent pumping problem occurs. If your Mono pump develops a fault or stops operating, contact our team to discuss the situation and arrange the appropriate response.
Experienced Pump Engineers
Mono progressing cavity pumps require an understanding of both the pump design and the material being transferred. Factors such as viscosity, solids content, abrasion and operating pressure all influence how a pump should be specified and maintained.
The experienced engineers at Mawdsleys Pump Services understand the importance of matching pumping equipment to its application. We can help assess your requirements, investigate performance problems and advise on suitable equipment for replacement or new installations.


Mono Pumps Sales FAQs
Mono pumps are used in a wide range of industrial and process applications, particularly where liquids are viscous, contain solids or are difficult to transfer using conventional pump designs. Common applications include wastewater treatment, sludge handling, food processing, chemical production, mining and agriculture.
A progressing cavity pump is a type of positive displacement pump that uses a rotating rotor inside a specially shaped stator. As the rotor turns, cavities move along the pump, carrying liquid from the inlet to the discharge. This produces a steady flow and makes the technology suitable for many viscous and solids-laden products.
Both are Mono progressing cavity pump ranges, but they have different design priorities. The EZstrip range incorporates a maintain-in-place arrangement to simplify maintenance without disconnecting the pump from its pipework. The Compact C range is designed around a compact construction for general industrial pumping duties. The best choice depends on the application, installation and maintenance requirements.
Yes. Mono manufactures specialist progressing cavity pumps for sludge-handling applications. Its Widethroat and EZstrip Cake pump configurations are particularly relevant to thick, high-solids materials, including dewatered sludge cake. The pump must be selected according to the material’s consistency, solids content and required operating conditions.
Mono offers hygienic progressing cavity pumps designed for suitable food and beverage applications. These can be used to transfer certain viscous and product-sensitive liquids. The required pump configuration will depend on the product, hygiene standards and cleaning procedures involved.
The easiest starting point is the information on the existing pump’s nameplate. The model designation, serial number and operating details can help identify the original equipment. It is also important to establish the required flow rate, pressure and characteristics of the liquid being pumped to ensure the replacement is suitable.